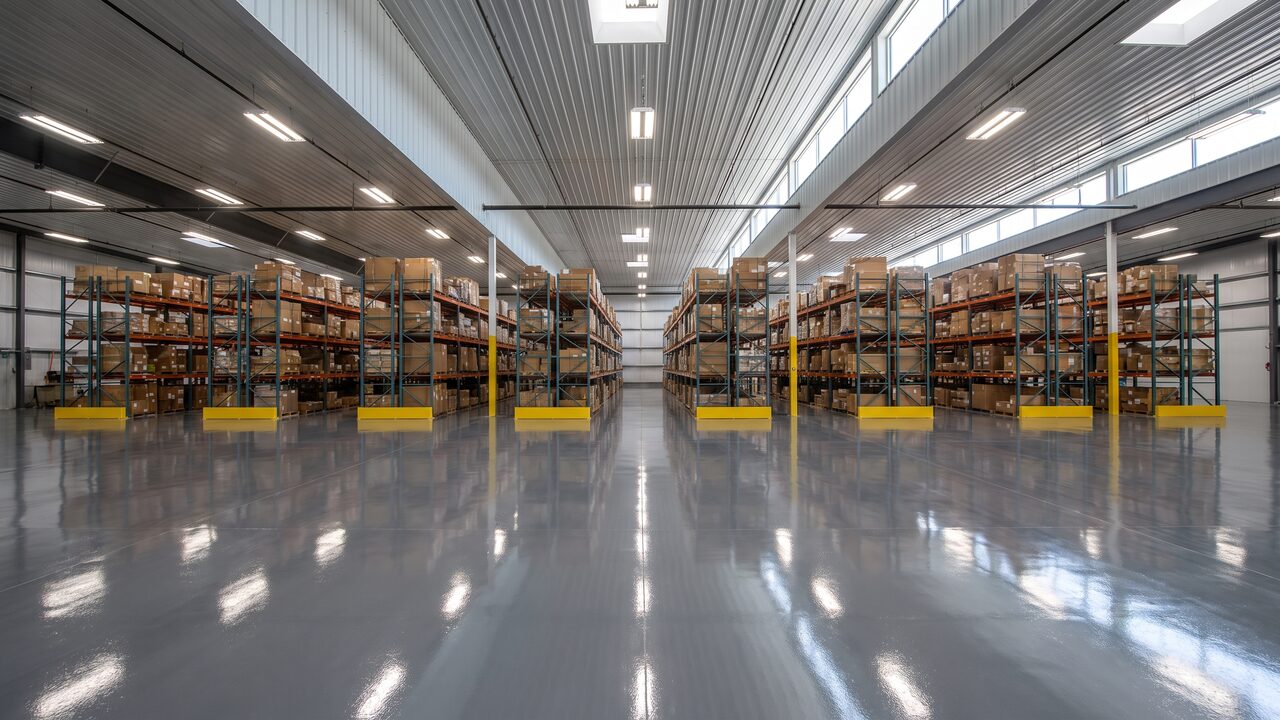
Any Phoenix distribution center handling electronic components needs to think about static control as part of its warehouse epoxy flooring Phoenix spec, not as an afterthought once the flooring is already installed. Electrostatic discharge (ESD) can destroy sensitive electronics with a charge too small for a person to even feel, and the floor is one of the primary paths that static charge travels through a facility.
This guide covers what ESD flooring actually requires under the governing industry standard, how to choose between the two main system types, and what ongoing testing looks like once a floor is installed.
Phoenix's rapid growth as a semiconductor and electronics manufacturing hub - driven by major fab investment across the metro over the past several years - has pulled a growing number of third-party logistics and distribution operators into the ESD compliance conversation for the first time. A facility that never needed to think about static control when it handled general retail goods now finds itself under contractual pressure to meet ESD standards the moment it starts handling electronics components or finished devices for a manufacturing client.
1. Why Static Control Matters in Distribution Centers
Static control matters because even a small electrostatic discharge - well below what a person can feel - is enough to damage or degrade sensitive electronic components, and a single undetected ESD event can create a defect that doesn't show up until the product fails in the field.
For a Phoenix distribution center handling electronics, semiconductor components, or assembled devices, an uncontrolled static environment isn't a minor operational nuisance - it's a direct product-quality and liability risk. Insurance and client contracts in the electronics supply chain increasingly require documented ESD compliance as a condition of doing business, which makes flooring spec a genuine business requirement, not just a technical preference.
The Cost of an Undetected ESD Event
What makes ESD damage particularly costly is that it's often invisible at the point of failure. A component can be zapped by a static discharge well within human-imperceptible range, pass initial functional testing, and then fail weeks or months later in the field - a phenomenon the industry calls "latent damage." For a Phoenix distribution or fulfillment operation, this means a static control failure on the warehouse floor might not show up as a rejected shipment or an obvious defect; it shows up as a warranty claim or a reliability complaint traced back through the supply chain, sometimes long after the product left the building.
2. ESD Flooring Standards: ANSI/ESD S20.20
ANSI/ESD S20.20 is the industry-standard program for protecting electrical and electronic parts, assemblies, and equipment from damaging levels of electrostatic discharge, and it defines the specific resistance ranges a facility's flooring must meet as part of a compliant static control program.
The standard doesn't just specify flooring in isolation - it covers footwear, workstations, grounding, and personnel practices as a complete system. But flooring is foundational, since it's the one element every person and every wheeled cart in the facility contacts continuously throughout the day. A facility can have excellent workstation-level ESD controls and still fail overall compliance if the floor itself doesn't meet spec.
ANSI/ESD S20.20 compliance is typically driven by one of two paths: a facility's own internal quality program mandates it as best practice, or a client contract in the electronics supply chain requires it as a condition of the business relationship. Either way, the standard expects a documented program - not just flooring installed to spec once and forgotten, but ongoing testing, training, and record-keeping that proves the static control system stays effective over time.
3. Conductive vs Static-Dissipative Epoxy Systems
Conductive epoxy systems drain static charge fastest and are specified for the highest-risk electronics handling zones, while static-dissipative systems offer a more moderate, controlled discharge rate that's the more common choice for general distribution center floors.
| System | Resistance Range | Best Use | Discharge Speed |
|---|---|---|---|
| Conductive epoxy | 10⁴-10⁶ ohms | High-risk electronics assembly, ESD-sensitive component handling | Fastest |
| Static-dissipative epoxy | 10⁶-10⁹ ohms | General distribution/fulfillment floors, mixed-use warehouses | Controlled, moderate |
| Standard (non-ESD) epoxy | 10⁹+ ohms (insulative) | No ESD requirement - standard commercial/industrial use | None - not rated for ESD |
The choice between the two ESD-rated systems typically comes down to the specific risk profile of what's being handled - a facility doing detailed board-level assembly or handling bare, unpackaged components generally specifies conductive, while a fulfillment center shipping fully-packaged finished electronics more often lands on static-dissipative as the balanced choice between protection and cost.
Both conductive and static-dissipative epoxy systems require a copper grounding grid embedded beneath the topcoat as part of the installation - this is what actually carries dissipated charge safely to the facility's electrical ground, and it's a step that can't be skipped or retrofitted easily after the fact. Planning ESD flooring alongside any electrical or racking work happening in the same phase of a build-out avoids costly rework later, since the grounding grid installation needs to happen before the final topcoat goes down.
4. Testing and Certifying Phoenix Warehouse ESD Floors
ESD flooring must be tested after installation and periodically thereafter to confirm it's actually performing within its specified resistance range - a floor that was compliant on install day can drift out of spec over time due to wear, contamination, or improper cleaning products.
Measures how well the floor conducts charge to the facility's grounding system - the core compliance measurement.
Tests resistance between two points on the floor surface, confirming consistent conductivity across the installed area.
Copper grounding strips embedded beneath conductive/dissipative flooring must maintain continuous, unbroken contact with the facility ground.
Test results should be logged and retained - many client contracts and audits require a documented testing history, not just a passing result on demand.
Annual testing is the ANSI/ESD S20.20 minimum, though high-throughput Phoenix distribution facilities with heavy cart and pallet traffic sometimes test more frequently in high-wear zones like dock doors and primary aisles where the floor sees the most abrasion.
It's worth budgeting for third-party ESD floor testing and certification as an ongoing operational cost, not a one-time installation expense. Many electronics-industry clients specifically require a third-party certification rather than a self-tested result, since an independent test carries more weight in an audit. Building this into your annual facilities budget from the start avoids a scramble later when a client or auditor asks for current documentation you don't have on hand.
5. Maintenance to Preserve ESD Performance Over Time
Maintaining ESD flooring performance requires cleaning products and procedures specifically compatible with conductive and static-dissipative systems - the wrong floor cleaner can leave an insulating residue that degrades the floor's conductivity even though the coating itself remains physically intact.
- Use ESD-compatible cleaners only - many standard industrial floor cleaners leave a film that raises surface resistance out of spec; always confirm compatibility before adding a product to your maintenance rotation.
- Avoid wax-based products entirely - floor wax is one of the most common causes of ESD floor failure during routine maintenance, since it forms an insulating layer over a conductive surface.
- Inspect high-wear zones regularly - dock doors, primary aisles, and workstation approach areas see the most foot and cart traffic and are the first places performance typically drifts.
- Re-test after any floor repair - patching or recoating a section of ESD flooring, even a small area, should trigger a re-test of that zone before it's returned to service.
- Train staff on footwear requirements - ESD flooring only completes the static-control loop when paired with ESD-rated footwear or heel straps in designated zones; a compliant floor with non-compliant footwear still allows static buildup on personnel.
Humidity control inside the facility itself is another maintenance lever worth considering in Phoenix specifically. Some distribution centers handling especially sensitive components add localized humidification in ESD-critical zones, since even a well-specified floor performs better as part of an environment where humidity isn't working against it. This is a facilities-engineering decision beyond flooring alone, but it's worth raising with whoever manages your ESD compliance program if static events are occurring more often than the flooring spec alone would predict.
If your existing warehouse floor needs a patch or partial recoat, our epoxy floor repair team understands the added care ESD-rated sections require compared to a standard commercial epoxy flooring repair. And if your facility's needs go beyond epoxy - for instance pairing ESD flooring zones with a polished concrete area in a showroom or office section - our concrete polishing team can help plan a facility-wide flooring strategy that keeps ESD-rated and non-rated zones clearly delineated. For the ESD system itself, our dedicated ESD anti-static epoxy page covers installation specifics in more depth.
6. Frequently Asked Questions
Get an ESD Flooring Assessment
Free consultation to determine the right ESD system and testing plan for your facility.